


Shandong Kosman Environmental Technology Co., Ltd. is one of the leading manufacturers and suppliers of integrated waste gas recovery unit in China. Please feel free to buy premium equipment for sale here and get pricelist from our factory. All customized products are with high quality and low price.
I. Product Overview
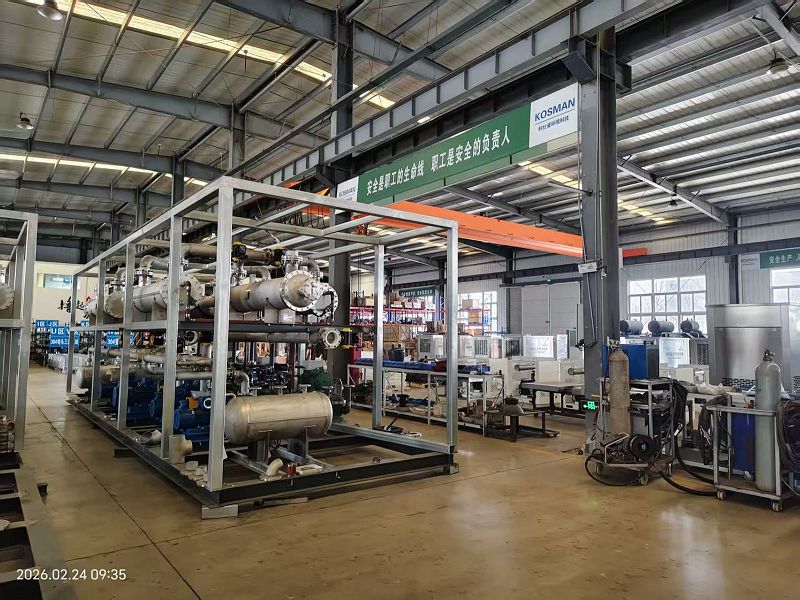
The integrated waste gas recovery unit is a comprehensive environmental protection system that highly integrates multiple VOC (Volatile Organic Compound) treatment technologies-such as condensation, adsorption, and membrane separation-into a single package. The unit consolidates process modules, control systems, and safety components onto a unified skid-mounted base; it is fully assembled and commissioned prior to shipment, requiring only power and gas line connections for on-site operation.
This product is designed primarily for high-concentration organic waste gas generated in industries such as chemicals, pharmaceuticals, electronics, coating, and petroleum storage and transportation. It employs a staged condensation process to liquefy and recover the majority of VOCs (achieving a solvent recovery rate of over 95%), followed by deep purification via adsorption or membrane separation units, thereby simultaneously achieving resource recovery and regulatory compliance for emissions.
Technical Positioning: For high-concentration organic waste gas (VOC concentration ≥ 1000 mg/m³), direct activated carbon adsorption results in bulky equipment and difficulty meeting emission standards, while direct incineration poses significant safety risks. The integrated waste gas recovery unit utilizes a "deep cryogenic condensation + post-treatment" staged process; it first recovers high-value solvents and drastically reduces waste gas concentration, then employs post-treatment facilities to ensure safe, compliant emissions.



II. Technical Principles and Process Flow
2.1 Core Operating Principles
The integrated waste gas recovery unit typically employs multi-stage condensation as its core process, supplemented by post-treatment units such as adsorption or membrane separation. The operating principles are as follows:
① Waste Gas Collection and Pre-cooling: Waste gas from various emission points is gathered via collection piping and enters a pre-cooler for initial cooling.
② Multi-stage Staged Condensation: The waste gas enters a deep cryogenic condensation system, where multi-stage cascade refrigeration progressively lowers the temperature to the design setpoint (adjustable between -25°C and -110°C). Hydrocarbon components with varying boiling points condense into liquid form sequentially. After gas-liquid separation, the condensate is automatically pumped into the user-designated storage tank.
③ Deep Purification Post-treatment (Optional): Uncondensed tail gas enters an activated carbon adsorption tank or a membrane separation unit for deep purification. Some units employ a dual-tank alternating adsorption design, where one tank undergoes desorption and regeneration while the other performs adsorption, ensuring continuous operation.
④ Compliant Discharge: Tail gas undergoes multi-stage treatment and is discharged only after testing confirms it meets emission standards.
2.2 Mainstream Process Routes
|
Process Route |
Technology Combination |
Applicable Scenarios |
Recovery Rate |
|
Condensation + Adsorption |
Multi-stage condensation/liquefaction recovery + activated carbon adsorption for deep purification |
High-concentration VOCs; ultra-low emission requirements |
≥95% |
|
Condensation + Membrane Separation |
Multi-stage condensation + selective separation via polymer membranes |
Medium-to-high concentrations; energy-consumption sensitive |
≥95% |
|
Condensation + Catalytic Combustion |
Multi-stage condensation recovery + catalytic oxidation/destruction |
Complex composition; off-gas with no recovery value |
≥95% |
III. System Composition
The integrated waste gas recovery unit primarily consists of the following components mounted on a skid base:
|
System Module |
Key Equipment/Components |
Functional Description |
System Module |
|
Condensing Unit |
Multi-stage compressor, condenser, evaporator, expansion valve |
Multi-stage cascade refrigeration; cools and condenses VOCs stage-by-stage |
Condensing Unit |
|
Gas-Liquid Separation Unit |
High-efficiency gas-liquid separator, recovered liquid storage tank |
Separates condensate from uncondensed gas; temporarily stores recovered solvent |
Gas-Liquid Separation Unit |
|
Adsorption/Post-treatment Unit |
Activated carbon adsorption tanks (dual-tank alternating operation), membrane module (optional) |
Deep purification of uncondensed tail gas; ensures emissions meet standards |
Adsorption/Post-treatment Unit |
|
Automatic Control System |
PLC control cabinet, explosion-proof instruments, touch screen |
Fully automatic control; real-time monitoring of parameters such as temperature and pressure |
Automatic Control System |
|
Skid-mounted Base |
Steel base, integrated frame |
Integrates all components into a single unit; facilitates transport and rapid installation |
Skid-mounted Base |
IV. Technical Parameters
|
Parameter/Item |
Technical Specifications |
|
Processing Capacity |
50–3,000+ Nm³/h (customizable) |
|
Condensation Temperature |
-25°C to -110°C (adjustable based on user requirements) |
|
Solvent Recovery Rate |
≥95% (typically exceeds 95%) |
|
Explosion-proof Rating |
Ex d IIB T4 / Ex dmbib IIB T4 |
|
Power Supply |
3-phase, 380V, 50Hz |
|
Control System |
Fully automatic PLC control; supports remote monitoring |
|
Product Configuration |
Skid-mounted |
|
Payback Period |
6–18 months |
V. Product Advantages
- High-efficiency recovery and cost-effectiveness: Solvent recovery rates exceed 95%; recovered high-value solvents can be directly reused in production, allowing the equipment investment to be recouped within 6 to 18 months.
- Staged treatment ensuring safety and compliance: High-concentration waste gas is first reduced to low concentration via deep-freeze condensation; subsequent treatment facilities then ensure compliant emissions while eliminating the safety risks associated with the direct incineration of high-concentration gas.
- Skid-mounted integration for rapid deployment: All units are integrated onto a skid base and pre-commissioned at the factory; on-site setup requires only the connection of utility lines (water, electricity, gas), resulting in a short installation period.
- Cold energy recovery for energy-efficient operation: Technologies such as cold energy recovery and staged condensation keep overall energy consumption at an optimal level.
- Fully automatic defrosting for continuous operation: Fully automatic defrosting technology and rapid condenser switching ensure stable, long-term operation.
- Explosion-proof design for safety and reliability: Designed and manufactured to explosion-proof standards (Ex d IIB T4), the equipment is suitable for both indoor and outdoor installation.
- Flexible processing capabilities: Operable across a 0–100% range, making it adaptable to intermittent emission scenarios such as loading operations.
VI. Application Scenarios
|
Application Sector |
Typical Scenarios |
Target Pollutants |
|
Chemical Industry |
Process exhaust from reactors, distillation, extraction, etc. |
Organic solvents such as benzenes, ketones, alcohols, and esters |
|
Pharmaceutical Industry |
Process exhaust, tank farm venting |
Methanol, ethanol, acetone, etc. |
|
Oil Storage & Transport |
Vapor recovery at gas stations, oil depots, and terminals |
Vapors from refined products like gasoline and aviation kerosene |
|
Refining & Petrochemical |
VOC control at loading racks and intermediate product tank farms |
Naphtha, aromatics, etc. |
|
Packaging & Printing |
Exhaust from printing, lamination, and coating processes |
Ethyl acetate, toluene, etc. |
|
Spray Painting Industry |
Exhaust from painting/coating lines |
Thinner, xylene, etc. |
|
Electronics Industry |
Exhaust from electronic component cleaning |
IPA, NMP, etc. |
Applicable exhaust gas conditions: High-concentration VOC exhaust streams (typically ≥1,000 mg/m³) with relatively simple compositions and recovery value.
VII. Selection Recommendations
|
Evaluation Criteria |
Recommended Conditions |
|
Exhaust Concentration |
High concentration (recommended ≥1000 mg/m³) |
|
Exhaust Composition |
Relatively simple composition; solvents have clear recovery value |
|
Emission Standards |
Must meet local environmental emission standards |
|
Airflow Capacity |
50–3000 Nm³/h (customizable based on requirements) |
|
Site Conditions |
Space-constrained; requires compact skid-mounted equipment |
|
Investment Payback |
Targeting rapid investment recovery (6–18 months) |
VIII. Ordering Information
|
Item |
Details |
|
Product Name |
Integrated Waste Gas Recovery Unit |
|
Process Options |
Condensation + Adsorption / Condensation + Membrane Separation / Condensation + Catalytic Combustion |
|
Processing Capacity |
50–3000+ Nm³/h (Customizable) |
|
Condensation Temperature |
-25°C to -110°C (Customizable) |
|
Explosion-proof Rating |
Ex d IIB T4 (Optional) |
|
Design Service Life |
≥10 years |
|
Warranty Period |
12–24 months |
|
Optional Configurations |
Online monitoring system, DCS communication interface, 4G remote O&M module, dual-channel anti-icing design |
|
After-sales Service |
Technical support, on-site response within 48 hours |
Specific prices and delivery times are subject to actual quotation.
IX. Contact Information
Please contact us for further product details, technical solutions, or to obtain a quote.
Hot Tags: integrated waste gas recovery unit, China integrated waste gas recovery unit manufacturers, suppliers, factory, combined fuel vapor recovery unit, combined refinery vapor recovery system, combined terminal vapor recovery system, common vapor recovery equipment, common vru unit, tank farm vapor recovery system