
Shandong Kosman Environmental Technology Co., Ltd. is one of the leading manufacturers and suppliers of Adsorption and Absorption Vapor Recovery System in China. Please feel free to buy premium equipment for sale here and get pricelist from our factory. All customized products are with high quality and low price.
I. Product Overview
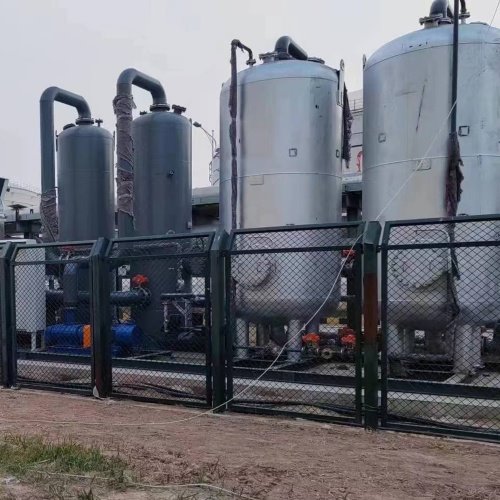
The combined Adsorption and Absorption Vapor Recovery System is a VOC (Volatile Organic Compound) treatment system that scientifically integrates adsorption and absorption technologies. The unit utilizes adsorption at the front end to concentrate hydrocarbon components from the Vapor stream, while employing absorption at the rear end to dissolve and recover the concentrated hydrocarbons, thereby achieving efficient separation of oil/gas vapors from the air.
This process represents the mainstream technical solution for high-throughput petroleum handling facilities (such as oil depots, refineries, and terminals). It has been widely deployed across 200 oil depots in regions including Beijing, Hebei, Shanghai, Zhejiang, and Guangdong, with a product series offering processing capacities ranging from 200 m³/h to 1,200 m³/h. The unit achieves a recovery rate of up to 99.6%, features minimal thermal effects in the adsorption tower, and maintains a carbon bed temperature rise of less than 35°C.
This product complies with the requirements of the *Emission Standard of Air Pollutants for Oil Depots* (GB 20950) and the *Technical Standard for Vapor Recovery and Treatment Facilities* (GB/T 50759-2022).
II. Technical Principles
2.1 Core Technical Principles
The unit separates volatile organic compounds (VOCs) from the air by leveraging the selective adsorption characteristics of adsorbents regarding hydrocarbon components. The core process flow is as follows:
- Adsorption Stage: Vapor vapors generated during loading/unloading or within the tank farm enter the activated carbon adsorption bed via a collection system; hydrocarbon components are adsorbed by the activated carbon, while clean air is discharged in compliance with standards.
- Desorption Stage: Once the adsorbent reaches saturation, a vacuum pump is used to create a vacuum (low vacuum level), desorbing the saturated hydrocarbons from the activated carbon.
- Absorption and Recovery: The desorbed, high-concentration Vapor vapors are conveyed to an absorption tower, where they are dissolved and absorbed by an absorbent medium (gasoline, diesel, or lean oil); the resulting rich oil is returned to the tank farm.
- Alternating Operation: The unit is equipped with two carbon beds that alternately undergo the "adsorption–desorption–regeneration" cycle, ensuring continuous 24-hour operation.
2 Process Flow Diagram
Tank farm/loading rack hydrocarbon vapors → Collection system → Carbon adsorption bed A (adsorption)
↓
Treated gas vented directly
↓
(Switch to carbon bed B upon saturation)
↓
Carbon adsorption bed A → Vacuum desorption → High-concentration hydrocarbon vapors → Absorption tower (lean oil/gasoline absorption)
↓
Rich oil returned to tank farm
↓
Activated carbon regeneration complete; ready for next switch
III. System Components
|
System Module |
Key Equipment/Components |
Functional Description |
|
Adsorption System |
Adsorption carbon beds (2 units, alternating operation), specialized activated carbon for vapor recovery |
Adsorbs hydrocarbon components from the vapor; purifies emissions to meet standards |
|
Desorption System |
Dry vacuum pump (staged variable-frequency regeneration) |
Extracts saturated vapors via vacuum to regenerate the activated carbon |
|
Absorption System |
Absorption tower (packed tower), lean oil pump, rich oil pump |
Uses gasoline, diesel, or lean oil to absorb high-concentration vapors |
|
Control System |
PLC control cabinet, online monitoring system, explosion-proof instrumentation |
Fully automated control; real-time monitoring of emission concentrations and operational data |
IV. Technical Parameters
|
Parameter Item |
Technical Specifications |
|
Processing Capacity |
100–2,500 m³/h (customizable) |
|
Vapor Recovery Efficiency |
≥99% |
|
Vapor Emission Concentration |
≤10 g/m³ |
|
Activated Carbon Type |
Specialized activated carbon for vapor recovery / Modified activated carbon |
|
Absorbent Type |
Gasoline / Diesel / Lean oil |
|
Design Service Life |
≥10 years |
|
Explosion-proof Rating |
Ex d IIB T4 (optional) |
|
Control Method |
Fully automatic PLC control; one-touch start/stop; supports online monitoring |
V. Product Advantages
- Extremely high recovery efficiency: Vapor recovery rates reach 99.6%, far exceeding the national standard requirement of ≥95%.
- Superior safety performance: Minimal thermal effects in the adsorption tower, with a carbon bed temperature rise of less than 35°C, making it safer than simple adsorption methods.
- Cost-effective investment: Integrated system investment is lower than that of simple absorption methods, offering significant overall benefits.
- Excellent emission performance: Emission concentrations can be as low as ≤10g/m³, outperforming the national standard of 25g/m³.
- Low energy consumption and easy maintenance: Utilizes dry vacuum pump technology with staged variable-frequency regeneration; both energy consumption and maintenance costs are lower than those of comparable products.
- Intelligent control: One-touch start/stop functionality with online monitoring of emission concentrations and operational data.
- Proven at scale: Widely deployed across 200 oil depots nationwide, recovering over 15,000 tons of gasoline annually.
VI. Application Scenarios
|
Application Areas |
Typical Scenarios |
|
Oil Depots/Storage Facilities |
Vapor recovery during loading at dispatch racks; treatment of storage tank breathing emissions |
|
Refining & Petrochemical Plants |
VOCs control at loading racks and intermediate product tank farms |
|
Chemical Plants |
VOCs control during chemical storage and transport |
|
Terminals/Docks |
Vapor recovery during ship loading operations |
Applicable media: Vapors from petroleum products (such as gasoline, naphtha, and aromatics like benzene, toluene, and xylene) and chemical products.
VII. Ordering Information
|
Item |
Details |
|
Product Name |
Adsorption and Absorption Vapor Recovery System |
|
Processing Capacity |
100–2,500 m³/h (customizable) |
|
Design Standards |
GB 20950, GB/T 50759-2022 |
|
Explosion-proof Rating |
Ex d IIB T4 (optional) |
|
Design Service Life |
≥10 years |
|
Warranty Period |
12–24 months |
|
Optional Configurations |
Online monitoring system, DCS communication interface, 4G remote O&M module |
|
After-sales Service |
Technical support; on-site response within 48 hours |
Specific prices and delivery times are subject to actual quotation.
IX. Contact Information
Please contact us for further product details, technical solutions, or to obtain a quote.
Hot Tags: Adsorption and Absorption Vapor Recovery System, China Adsorption and Absorption Vapor Recovery System manufacturers, suppliers, factory, activated carbon vapor recovery skid, adsorption vapor recovery equipment package, adsorption vapor recovery skid, carbon bed vapor recovery equipment, gasoline carbon adsorption unit, petroleum carbon adsorption unit